Intelligent system solutions

Here is the title one h1 placeholder text
- Product description
- Model specifications
- Product Features
- Other instructions
-
- Commodity name: Chocolate Factory Management System

Case Background
Cadbury is a world-renowned candy manufacturer with a history of 200years that has introduced MH-SCADA in its chocolate product processing factory to help achieve comprehensive integrated management.
Case Analysis
The chocolate factory employs a fully automated production method, with human involvement only in the first process—raw material input and the last process—quality inspection sampling, while all other production processes are completed by advanced automated equipment.

Various raw material powders used for making chocolate are transported from the powder silo to the powder processing system, weighed according to the product formula, and then enter the reactor through a valve. Correspondingly, ingredients such as fats, cocoa mass, and water are also added to the reactor through their respective independent transport routes, where the reactor fully mixes these raw materials into a paste. The refiner refines this paste into small flakes, which are then shaped into various chocolate products.
The entire chocolate factory is controlled by 8sets of Allen Bradley PLCs, one set for overall monitoring, and another 6 sets distributed across different powder silos, responsible for controlling the operation of production equipment. Additionally, one PLC is connected to the powder processing system and the refiner to control the operation of these devices. The PLCs communicate with each other via Allen Bradley's DeviceNet fieldbus to collaboratively complete control functions.

The MH-SCADA system connects all PLCs in the factory via Ethernet, and the entire SCADA system uses approximately 50,000 scanning tags.
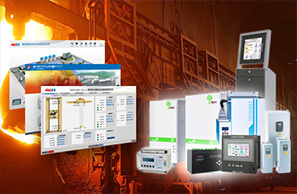
MH-SCADA features a distinctive vector graphic tool, and the monitoring system used on-site utilizes this tool to directly reflect the mechanical status of on-site equipment, operational parameter data, fault feedback information, etc., in graphical form, and provides real-time video monitoring of certain key production steps on a large screen, vividly reflecting the operational status of on-site equipment.
The MH-SCADA software can record alarm analysis data from on-site equipment, different chocolate product formula data, as well as important information such as raw material weighing data and product batch numbers into an SQLdatabase, and can generate corresponding analysis and statistical reports based on user needs. In the monitoring system, these reports are in WEB page format, making it very convenient to view using a client, and they can also be exported to documents in formats such as Excel for regular backups.
This SCADAsystem uses a set (two) of redundant servers to ensure data security and continuity. In addition to production line equipment, the factory also uses MH-SCADA software as a monitoring platform for the boiler system.
User Benefits
In the chocolate production process, even a small error can lead to significant cost losses and raw material waste. The MH-SCADAsystem provides sufficient safety guarantees for on-site production operations, greatly improving the utilization rate of chocolate raw materials and saving a large amount of production costs.
At the same time, adopting a highly automated production process and using MH-SCADAas an effective production monitoring system also saves a lot of labor costs for hiring production personnel and equipment maintenance staff.